
Liquid ring
vacuum pumps
Reliable vacuum generation even with demanding media.
Areas of applications
- Liquid ring vacuum pumps are compressors used for vacuum generation and are employed across a wide range of industries for suction, leakage extraction and degassing, including process engineering, the chemical industry, food processing, energy supply and mechanical engineering
- Suitable for dry, saturated and contaminated gases, vapours and entrained liquids while maintaining a constant vacuum
- Specially designed versions are also suitable for explosive gases such as hydrogen
- Particularly suitable for small, compact and customised vacuum systems (e.g. UniVac)
- Oil-free compression with no oil in the pumped medium or exhaust air
- Suction pressures down to 33 mbar abs., and down to 5 mbar abs. with gas ejectors or jet compressors
- RoHS II-compliant versions in accordance with Directive 2011/65/EU and Delegated Directive (EU) 2015/
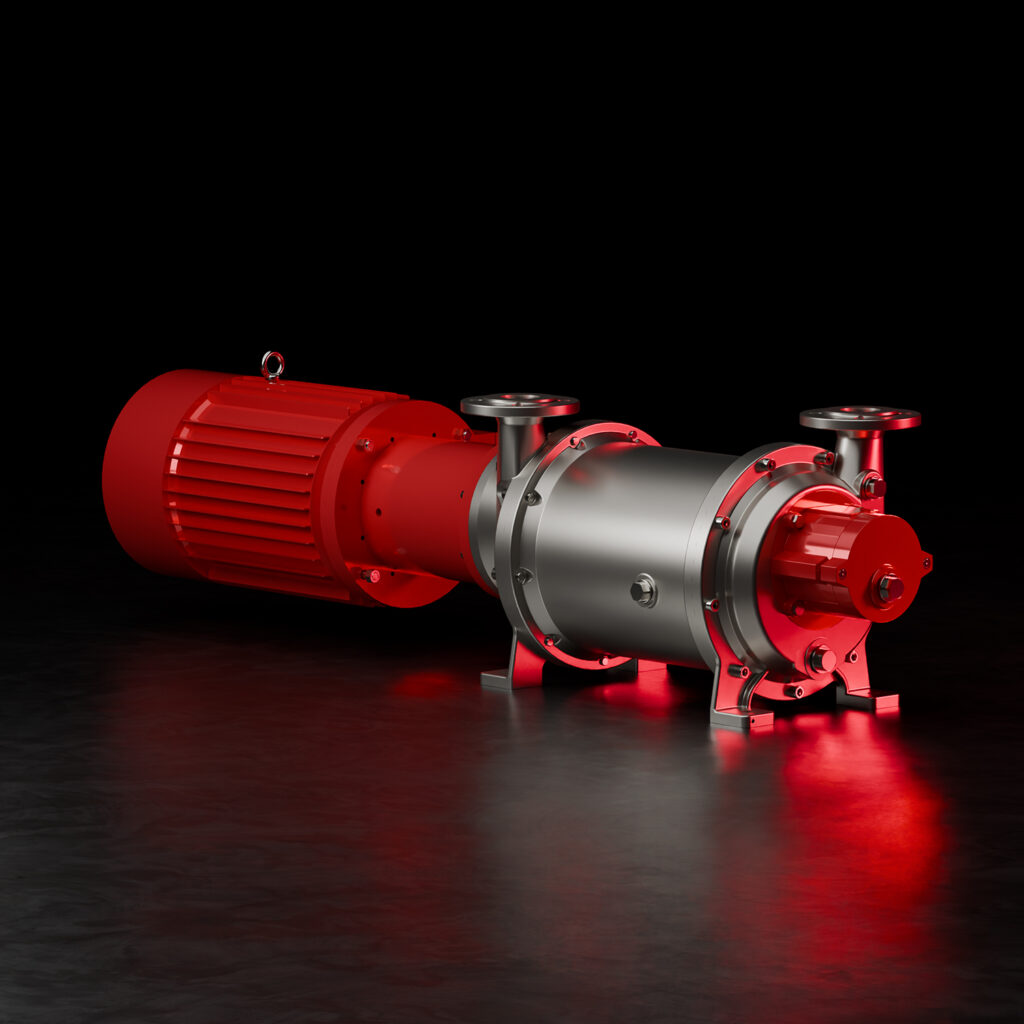
Design
- Liquid ring vacuum pumps operate with an eccentrically mounted impeller and a liquid ring as the sealing element; together with the impeller blades, this creates working chambers with varying volumes that generate the vacuum
- Robust design with few moving parts and correspondingly low wear
- Single-stage or two-stage design for different vacuum requirements; operation with water or suitable process liquids
- Manufactured in grey cast iron, brass, bronze, stainless steel, duplex and super duplex stainless steel, Hastelloy and other special materials; material selection depends on the pumped medium, operating liquid, temperature, corrosion and process conditions
- Connection options with DIN and ANSI flanges as well as G and NPT threads
- Coating systems with ACC cathodic dip coating as well as special coatings available upon request
Liquid ring vacuum pumps
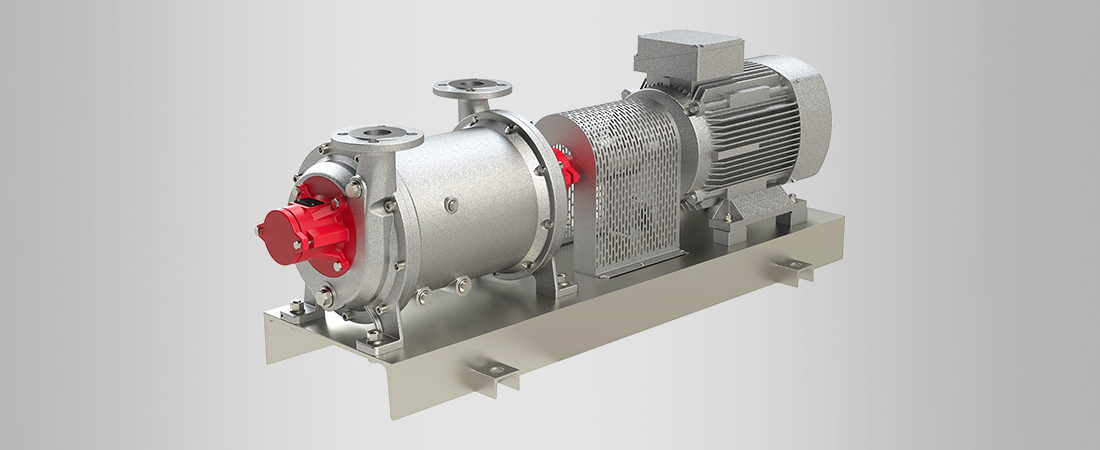
Advantages
- High operational reliability even with moist and condensing gases
- High suction capacity due to the condensation of condensable vapours in the liquid ring
- Insensitive to liquid content in the pumped medium
- Smooth running and low vibration levels
- Special solutions and customised designs tailored to the specific application and process requirements
- Flexible choice of materials, connections, coating systems and design variants
- ATEX versions for use in potentially explosive atmospheres
Description
- Circutec liquid ring vacuum pumps for vacuum generation when handling air, gases and vapours
- Single-stage versions for high pumping capacities and two-stage versions for higher vacuum requirements
- Operating liquid: water or suitable process liquids, depending on the application and design
- Robust design for reliable continuous operation and long service life
- Available with single mechanical seal, stuffing box packing, double mechanical seal with flushing system, or magnetic coupling with low-loss containment shell
- Casing seals with O-rings, flat gaskets, liquid sealants or PTFE tape
- Pump and vacuum system design according to the pumped medium, operating liquid, vacuum level, temperature, material requirements and operating conditions
- ATEX versions for potentially explosive atmospheres in accordance with the specific application and zone classification
- Depending on the version, the unit can be supplied with ATEX marking up to II 1/2G Ex IIB + H2/IIC T4…T1 Ga/Gb X
UniVac – our compact vacuum system
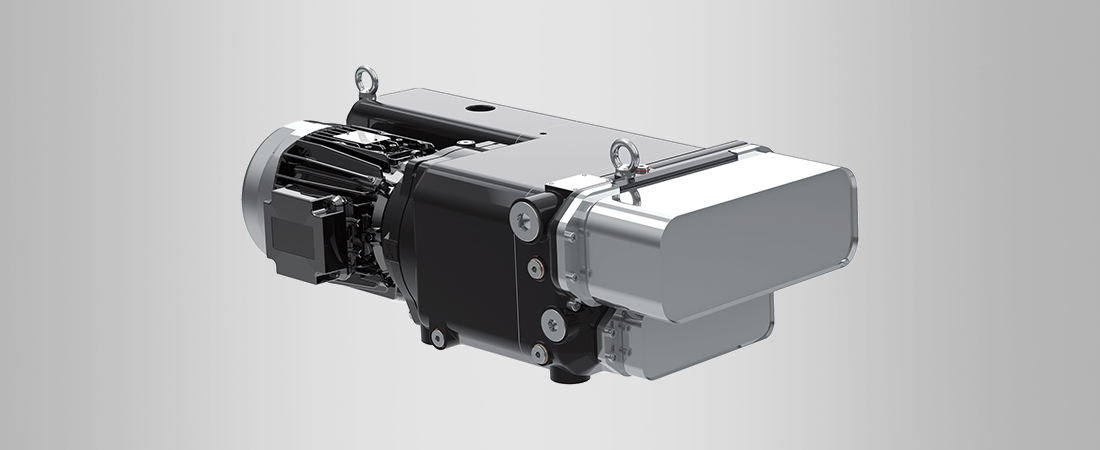
Advantages
- Mechanically ready-to-connect plug-and-play vacuum units – developed for sterilizers
- Also suitable for degassing, drying and distillation
- Extremely compact, fully pre-assembled and easy to maintain
- Highly efficient two-stage separator
- Efficient IE3 and IE4 motors with variable frequency control
Description
- Vacuum units comprising liquid ring vacuum pumps, separator, condenser and optional heat exchanger
- Integration of additional components such as gas ejectors, valve technology, sensors or exhaust gas condensers available upon request
- UniVac-…-2 with quiet two-stage vacuum pumps from the VZ series
- UniVac-10 as a compact system with air cooler
- Cost-effective grey cast iron version with ACC / cathodic dip coating
Custom vacuum systems
We are also pleased to offer comprehensive vacuum systems for all of our liquid ring vacuum pumps, individually tailored to your specific requirements.
Upon request, the scope of supply may include, for example, liquid ring vacuum pumps with:
- Discharge pump for circulating the operating liquid
- Heat exchanger (plate heat exchanger or shell-and-tube heat exchanger) for cooling the operating liquid in a closed-loop cooling system
- Condenser for pre-condensation on the suction side of the liquid ring vacuum pump
- Stainless steel separator tank on the discharge side for separating the liquid-gas mixture and returning the operating liquid
- Ball check valve installed on the suction side to prevent backflow into the process
- Circutec gas ejector matched to the liquid ring vacuum pump for achieving lower ultimate pressures
- Stainless steel piping between all components, including operating liquid line, cavitation protection line and motive gas line
- Installation on a baseplate or customised base frame made of steel or stainless steel
- Installed flushing systems for double mechanical seals
- Installed sensors, particularly for ATEX applications up to 1G/2G, e.g. for level, pressure, temperature and flow monitoring
- Ball valves and solenoid valves
- Level indicators
- Modified pump connections, e.g. for external flushing systems or vibration measurements
- Customised gas ejector for operation with higher operating water temperatures